Series 100i
Cost-Effective, Compact, and Easy-to-Operate Palletizing Automation
The Automated Industrial Tech Series 100i Single Chamber Palletizer is a cost-effective solution for businesses looking to improve packaging-line efficiency and automate end-of-line palletizing. Designed with a compact footprint, straightforward operation, and reliable industrial components, the Series 100i helps to simplify the process of stacking packaged products onto pallets while reducing the demands of manual handling.
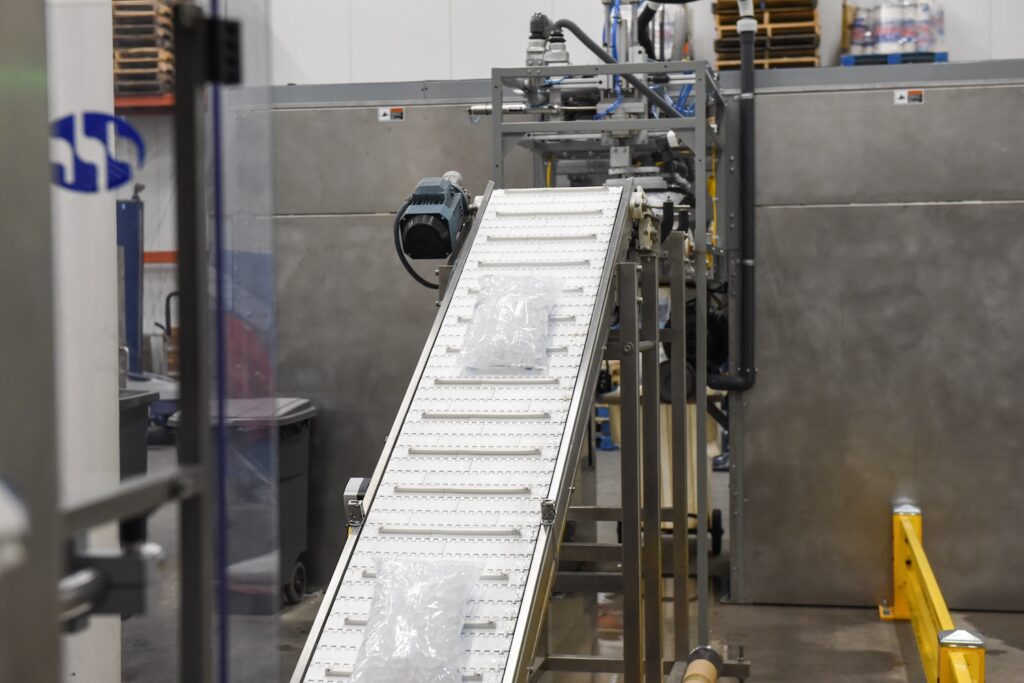
Capable of handling cases, bags, and trays weighing up to 50 pounds, the Series 100i is well suited for a variety of industries, including packaged ice, fertilizer, mulch, pellet fuel, beverages, and other packaged goods. Depending on package size, the system can palletize approximately 35–40 bags per minute with a pallet change-out time of less than one minute, helping businesses keep pace with production demands.
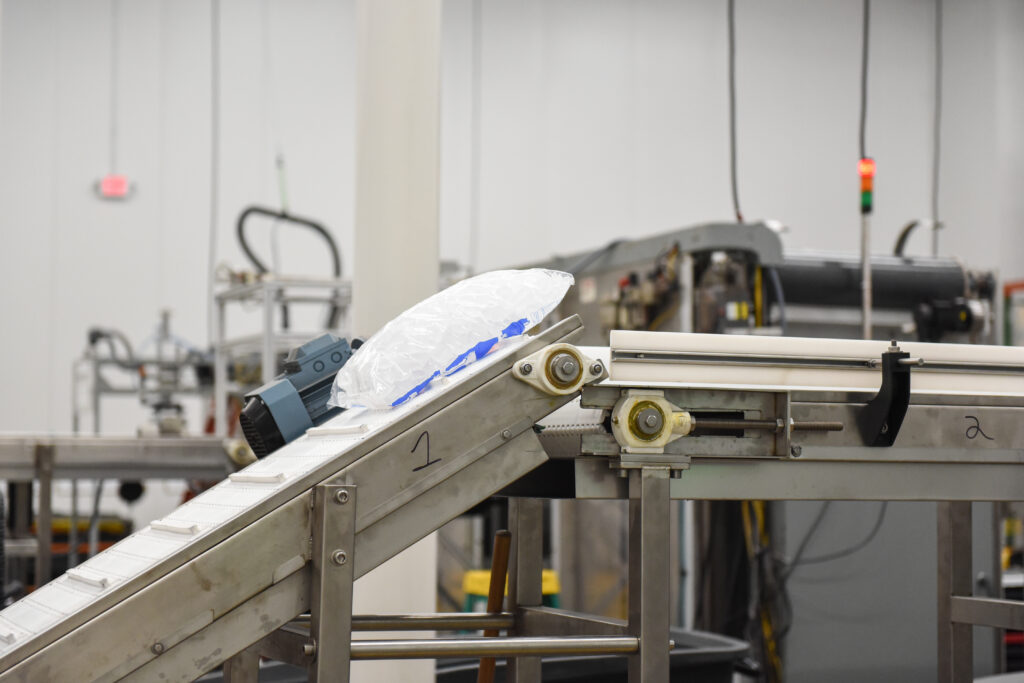
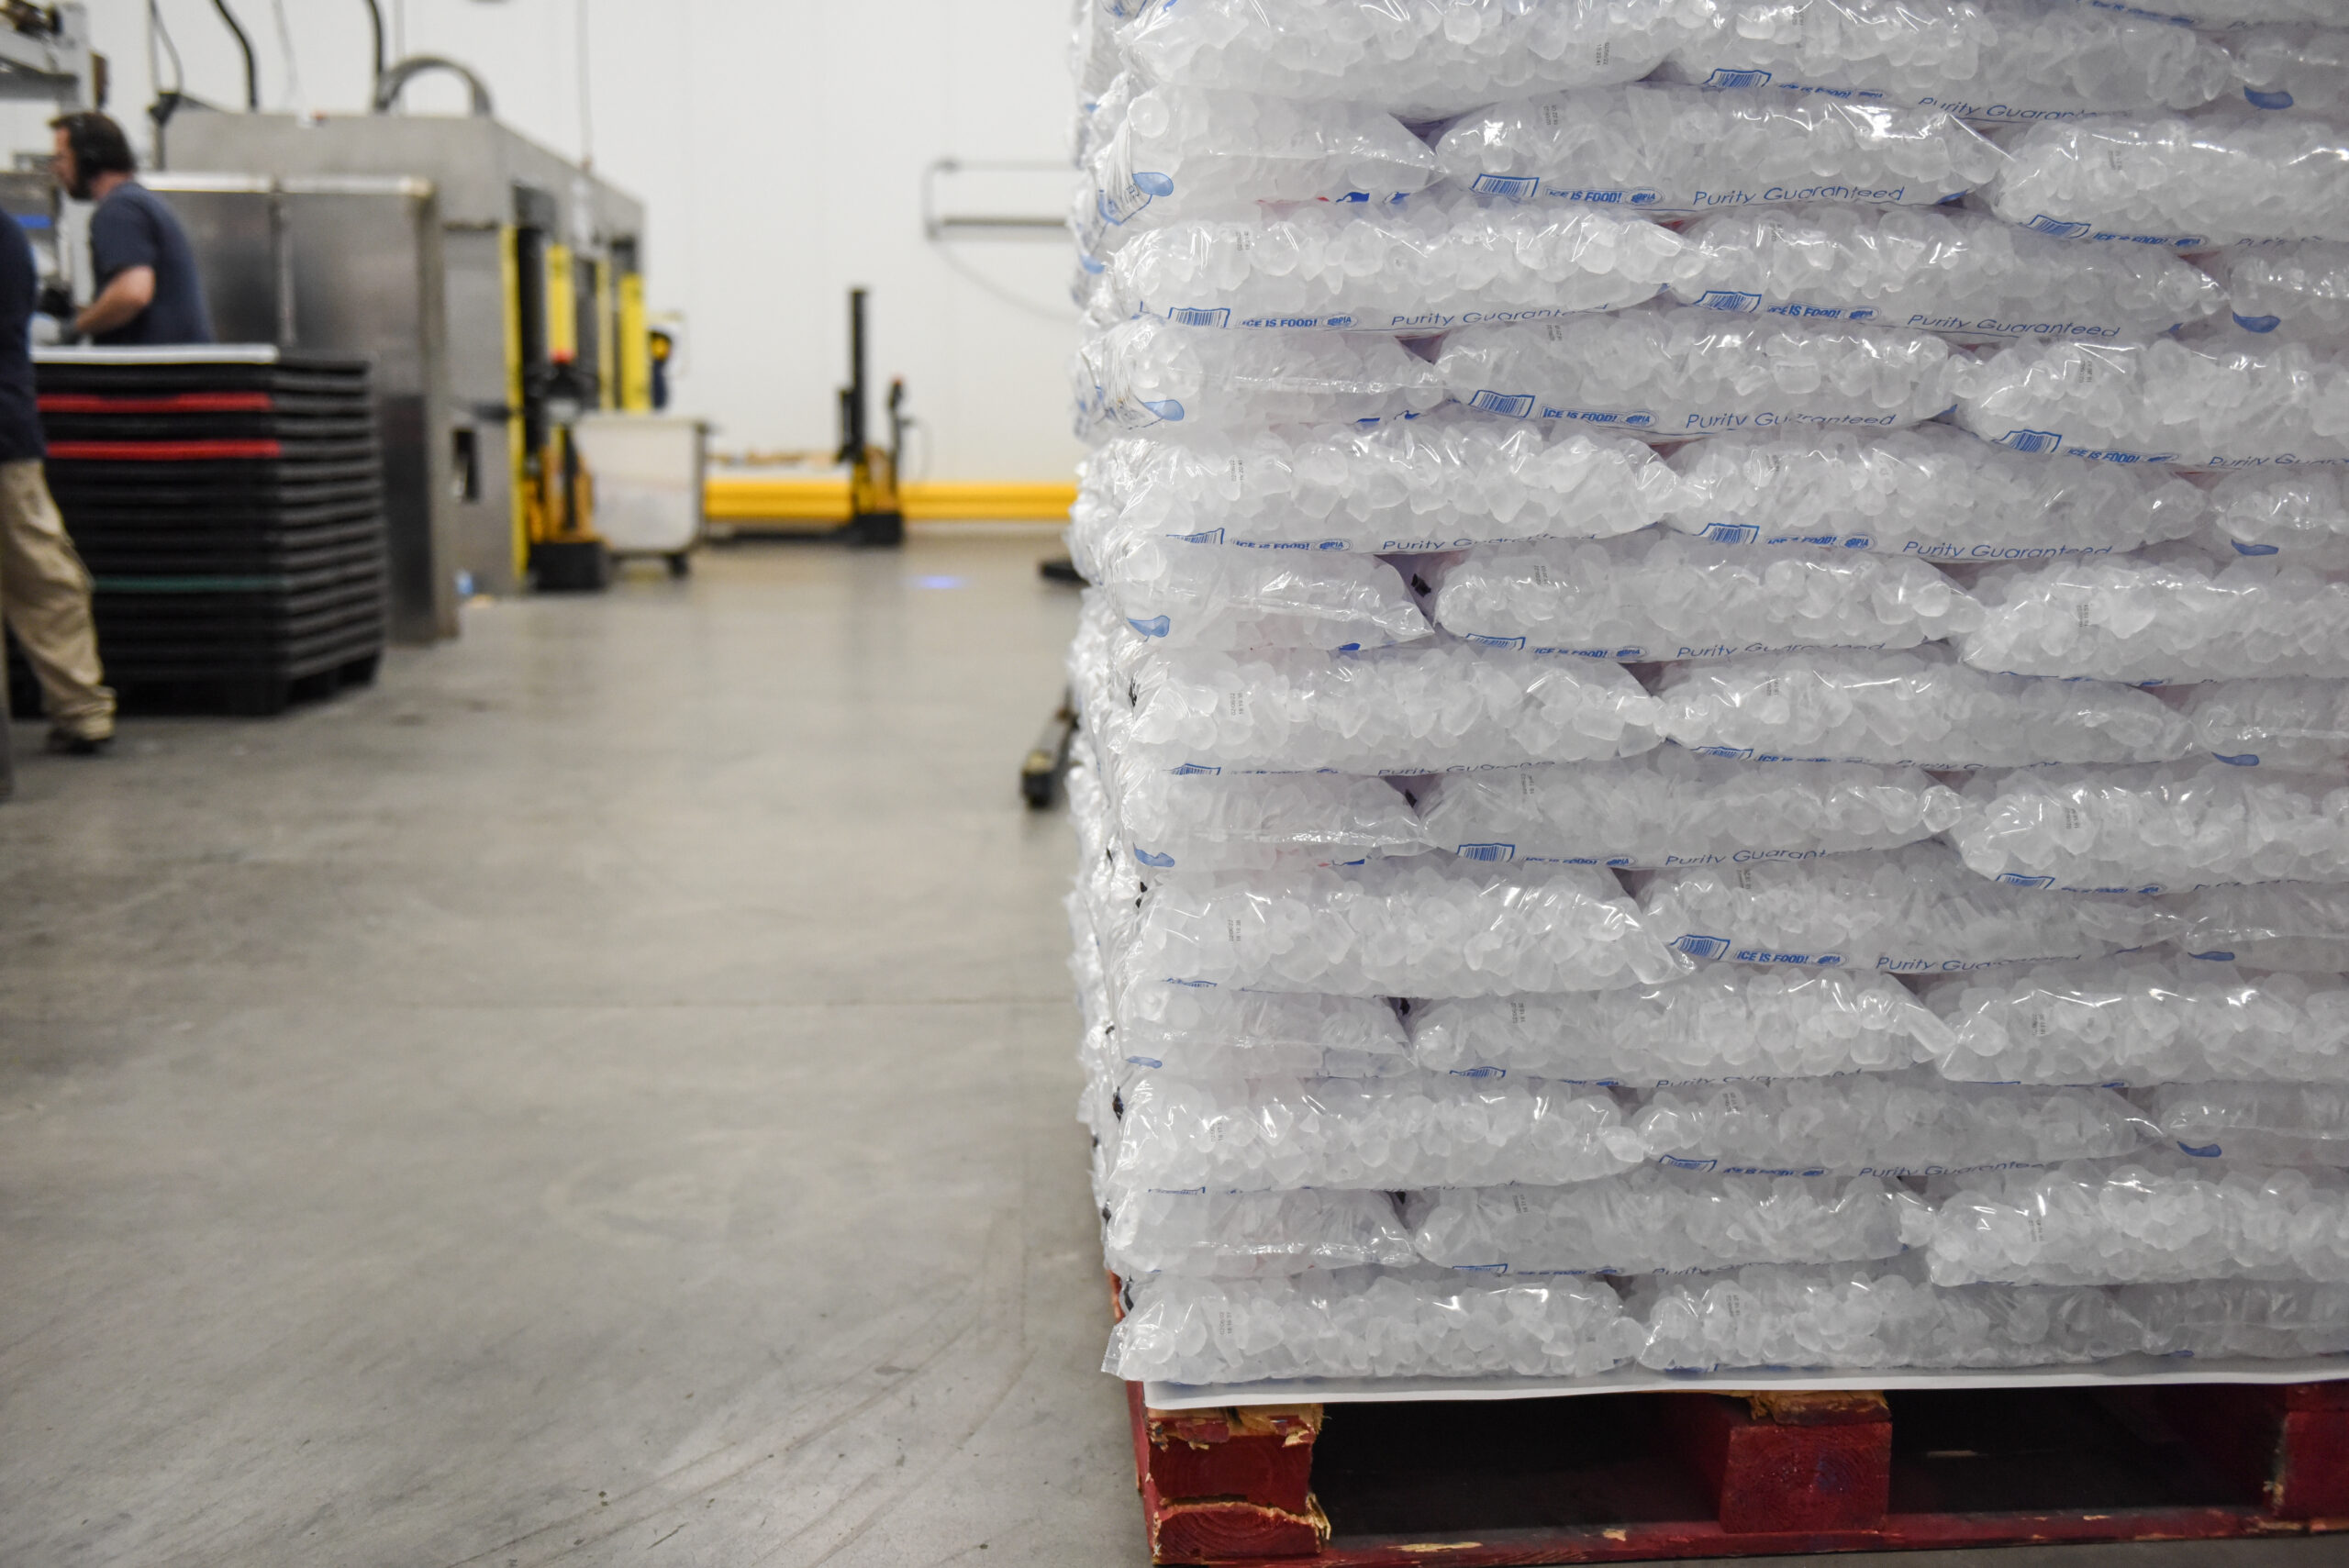
Built for dependable performance and ease of use, the Series 100i features a powder-coated steel construction, servo controls for speed and accuracy, and a PLC with touchscreen controls. An automatic product-reject system removes faulty packages from the palletizing process, while upstream equipment communication helps the machine work alongside other packaging-line equipment. Remote diagnostics and program changes are also supported through its web server.
For businesses seeking a practical entry point into palletizing automation, the Series 100i combines proven design principles with serviceable, brand-name components. Its single-chamber configuration can also be converted to a dual-chamber arrangement, providing a potential upgrade path as operational needs evolve.
The Series 100i operates on 230/480V three-phase power and has a low compressed-air consumption of approximately 5–6 SCFM.
Whether you’re handling packaged ice, bagged fertilizer, mulch, pellet fuel, or other packaged products, the Automated Industrial Tech Series 100i offers a practical way to streamline palletizing, improve production flow, and take the next step toward automation.
Contact Automated Industrial Tech to discuss your application and determine whether the Series 100i is the right palletizing solution for your operation.